
 EN


The Evolution of Global Material Handling Supply Chains
Over the past decade of consulting extensively with international distribution centers, automated fulfillment hubs, and major warehouse facility operators across North America, Western Europe, and Southeast Asia, one recurring operational truth has become glaringly obvious: the reliability and performance consistency of your material handling fleet directly dictates the operational velocity of your entire enterprise. When global supply chains face sudden, unpredictable spikes in consumer purchasing demand or seasonal e-commerce rushes, warehouse managers and logistics directors simply cannot afford unexpected equipment downtime caused by substandard manufacturing or faulty components. Drawing from hands-on factory floor audits, supply chain evaluations, and direct executive consultations, the traditional commercial approach of sourcing generic machinery through multiple layers of distant third-party intermediaries is rapidly fading into obsolescence. Today's forward-thinking logistics leaders are actively seeking direct, transparent partnerships with an established, reputable forklift supplier equipped to deliver dependable, high-performance machinery tailored precisely to their unique operational environments without ever compromising on structural integrity or safety standards. Establishing a direct manufacturer relationship eliminates unnecessary markups and ensures direct technical communication from the production floor to the end-user.
Technical Mastery: Core Engineering and Manufacturing Standards
Achieving exceptional long-term durability and structural reliability within high-intensity, multi-shift warehouse environments requires uncompromising mechanical, electrical, and hydraulic engineering. Modern heavy-duty material handling machinery must integrate high-precision electric alternating current drive systems, robust hydraulic lifting cylinders, and reinforced high-grade steel chassis configurations capable of absorbing continuous operational stress day in and day out. Unlike standard commercial vehicles that operate in open spaces, industrial forklifts undergo severe thermal cycling, heavy dynamic loading, and rigorous physical strain during everyday lifting, high-tier stacking, and long-distance transporting cycles. Advanced manufacturing facilities leverage cutting-edge automated laser cutting technology, robotic precision welding, and comprehensive computer-controlled stress-testing protocols to ensure that every individual component—from the overhead guard and counterweight down to the steering axle and fork carriage—meets the most rigorous international structural tolerances. This meticulous engineering precision directly translates into smoother acceleration, optimized energy conservation, and greatly extended vehicle lifespans when operating under heavy industrial loads in demanding facilities.
Industry Benchmarks and Global Compliance
When enterprise-level procurement buyers evaluate global machinery manufacturers, strict adherence to internationally recognized safety certifications, quality benchmarks, and regulatory frameworks is entirely non-negotiable. Governing bodies, trade organizations, and standardization authorities, such as the International Organization for Standardization and the European conformity directives, explicitly dictate that industrial lifting equipment must undergo exhaustive validation and testing before ever entering the commercial market. A reputable global supplier maintains stringent internal quality control systems that seamlessly align with these global benchmarks, ensuring complete transparency regarding raw material sourcing, brake system reliability, and advanced mast stability tests. By complying with these rigorous safety frameworks, manufacturers actively protect frontline warehouse operators from workplace hazards while guaranteeing that equipment operates smoothly within heavily regulated international warehouse facilities, thereby minimizing legal liabilities and operational risks for business owners. Furthermore, certified compliance serves as an immediate and trustworthy indicator of a manufacturer's dedication to uncompromising operational excellence across global markets.
Economic ROI and TCO in Equipment Sourcing
Investing in heavy industrial machinery requires a disciplined, data-driven financial approach that looks far beyond the initial equipment purchase price. When calculating the comprehensive total cost of ownership for a commercial forklift fleet over its operational lifetime, facility directors and financial controllers must carefully factor in maintenance frequency, energy consumption rates, spare parts availability, and expected residual resale value. While low-cost, unverified machinery alternatives may look appealing on initial capital expenditure spreadsheets, they frequently incur skyrocketing maintenance repair bills, frequent component failures, and excessive operational downtime that cripples productivity. Premium engineered equipment designed with modular components and energy-efficient lithium-ion or advanced lead-acid battery configurations dramatically lowers ongoing maintenance expenditures. This perfect balance of upfront efficiency and long-term mechanical durability ensures rapid capital payback and sustained operational profitability across multi-year asset lifecycles, ultimately protecting corporate bottom lines and maximizing overall return on investment for stakeholders globally.
Empowering Global Logistics with Huahe
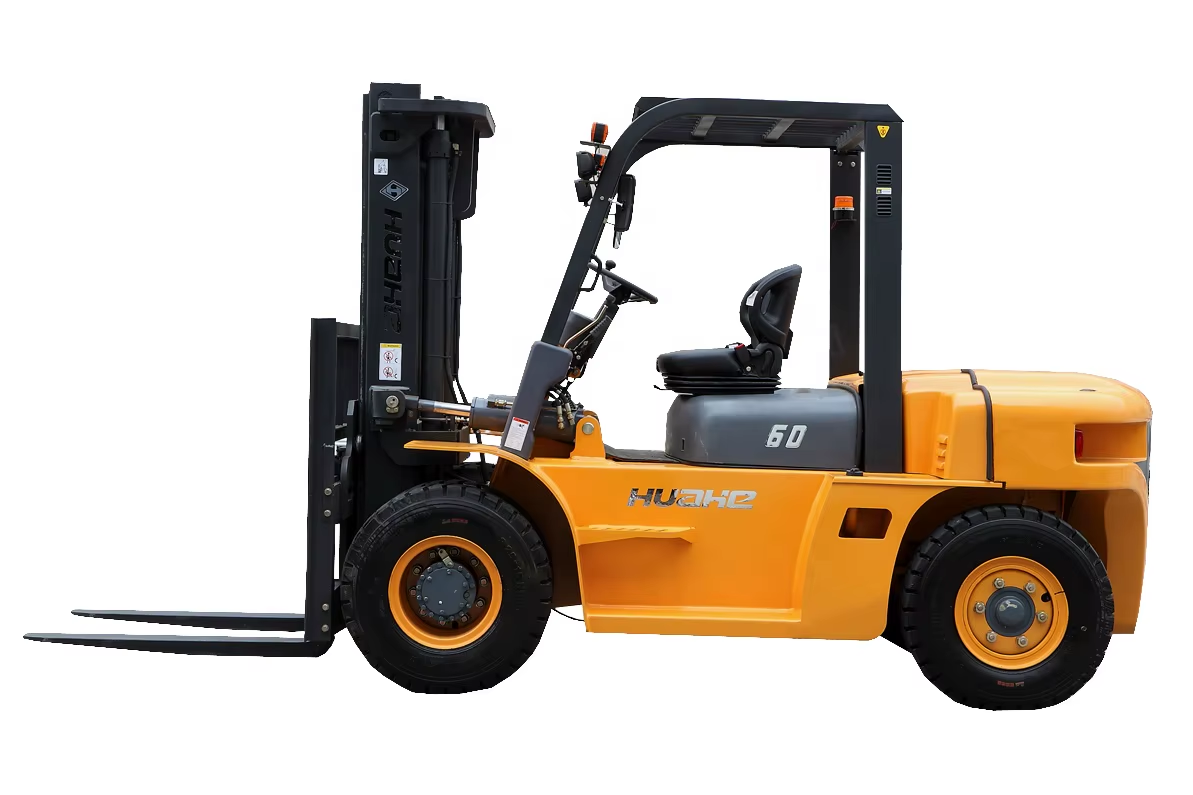
Navigating the complexities of international trade and heavy equipment procurement demands a reliable manufacturing partner who deeply understands both technical production scale and flexible custom adaptability. Huahe stands firmly at the forefront of this industrial sector, leveraging state-of-the-art production lines, rigorous quality management systems, and advanced research and development capabilities to deliver world-class material handling solutions. By providing comprehensive OEM and ODM manufacturing services, Huahe empowers global logistics enterprises, regional distributors, and warehouse operators with tailor-made machinery engineered specifically to withstand demanding operational schedules. Partnering with Huahe means investing directly in manufacturing excellence, dependable global supply chain support, and a future-proof foundation designed to elevate your warehouse productivity to unprecedented heights across worldwide markets, ensuring long-term success in an increasingly competitive global economy. Through continuous product innovation, rigorous quality control, and unwavering dedication, Huahe remains your trusted ally in modern material handling and logistics optimization.